Why Your Python-Embossed or Crocodile-Embossed Leather Pumps Show Visible Pattern Wear, Scuff Marks, and Smooth-Underlayer Exposure at the Toe Box and Heel Strike Zone After Only a Few Months
She bought the burgundy python-embossed leather curved pumps for the autumn cocktail party because the listing photo showed a deep, sculptural snake-scale pattern across the entire vamp with the marketing phrase "premium embossed leather with sculptural scale pattern that holds its dimensional depth wear after wear." The first two wears were stunning — the burgundy scales sat crisp and dimensional across the metatarsal zone, the snake-scale pattern caught the candlelight at every step, and the curved pumps were the most distinctive pair on her cocktail shoe rack. By month three she noticed a 4-6 mm scuff at the lateral-side toe-edge where the scales had visibly flattened — the once-crisp scale-edge profile had worn smooth to the touch, and the smooth underlying burgundy leather was visible in a 2-3 mm band along the toe-edge. By month four the scuff zone had widened to 12-18 mm, the scale-edge profile at the toe-box had flattened by 60-75% across the entire ball-of-foot zone, and a faint 4-6 mm smooth band was visible at the heel-strike zone where the right-foot heel-strike had abraded the scale-edge profile to the underlying leather. By month six the toe-box and heel-strike zones showed 28-42 mm scrnee-to-smooth exposure, the once-sculptural snake-scale pattern had lost 60-75% of its dimensional depth across the entire vamp, and the smooth underlying burgundy leather was visible from across the room at the cocktail bar. The burgundy python-embossed leather pumps she paid $195 for had surrendered the emboss-pattern depth within six months because the factory had specified a 38-52 kg/cm² emboss-plate pressure at 0.6-0.8 mm emboss-depth producing 72% pattern-wear incidence, a 0.6-0.9% compression-set at the emboss-peak zone flattening the scale-edge by 38-58% at month 3, an 18-26 micron polyurethane top-coat with 22-26% plasticizer content scuffing at 12-22 wear cycles, and no moisture-blocking 2-coat primer allowing 0.6-0.9% foot-sweat lipid saturation to hydrolyze the emboss-pattern edge-bond at month 3. The four construction choices that saved the factory $3.65-6.85 per pair in emboss labor and top-coat material were also the four construction choices that drove the emboss-pattern-wear failure that destroyed the sculptural dimensional depth of the burgundy python-embossed leather pumps within six months. A construction choice that costs the customer an extra $7.45-13.85 per pair to upgrade at the factory floor, and that the mass-market supply chain has standardized on because the buying public judges embossed leather shoe construction from the listing phrase "sculptural embossed pattern" rather than from the emboss-plate pressure, emboss-depth geometry, top-coat thickness, and primer chemistry that actually determine whether the emboss-pattern will hold its dimensional depth for twenty-four months or scuff to the smooth underlying leather within six months.
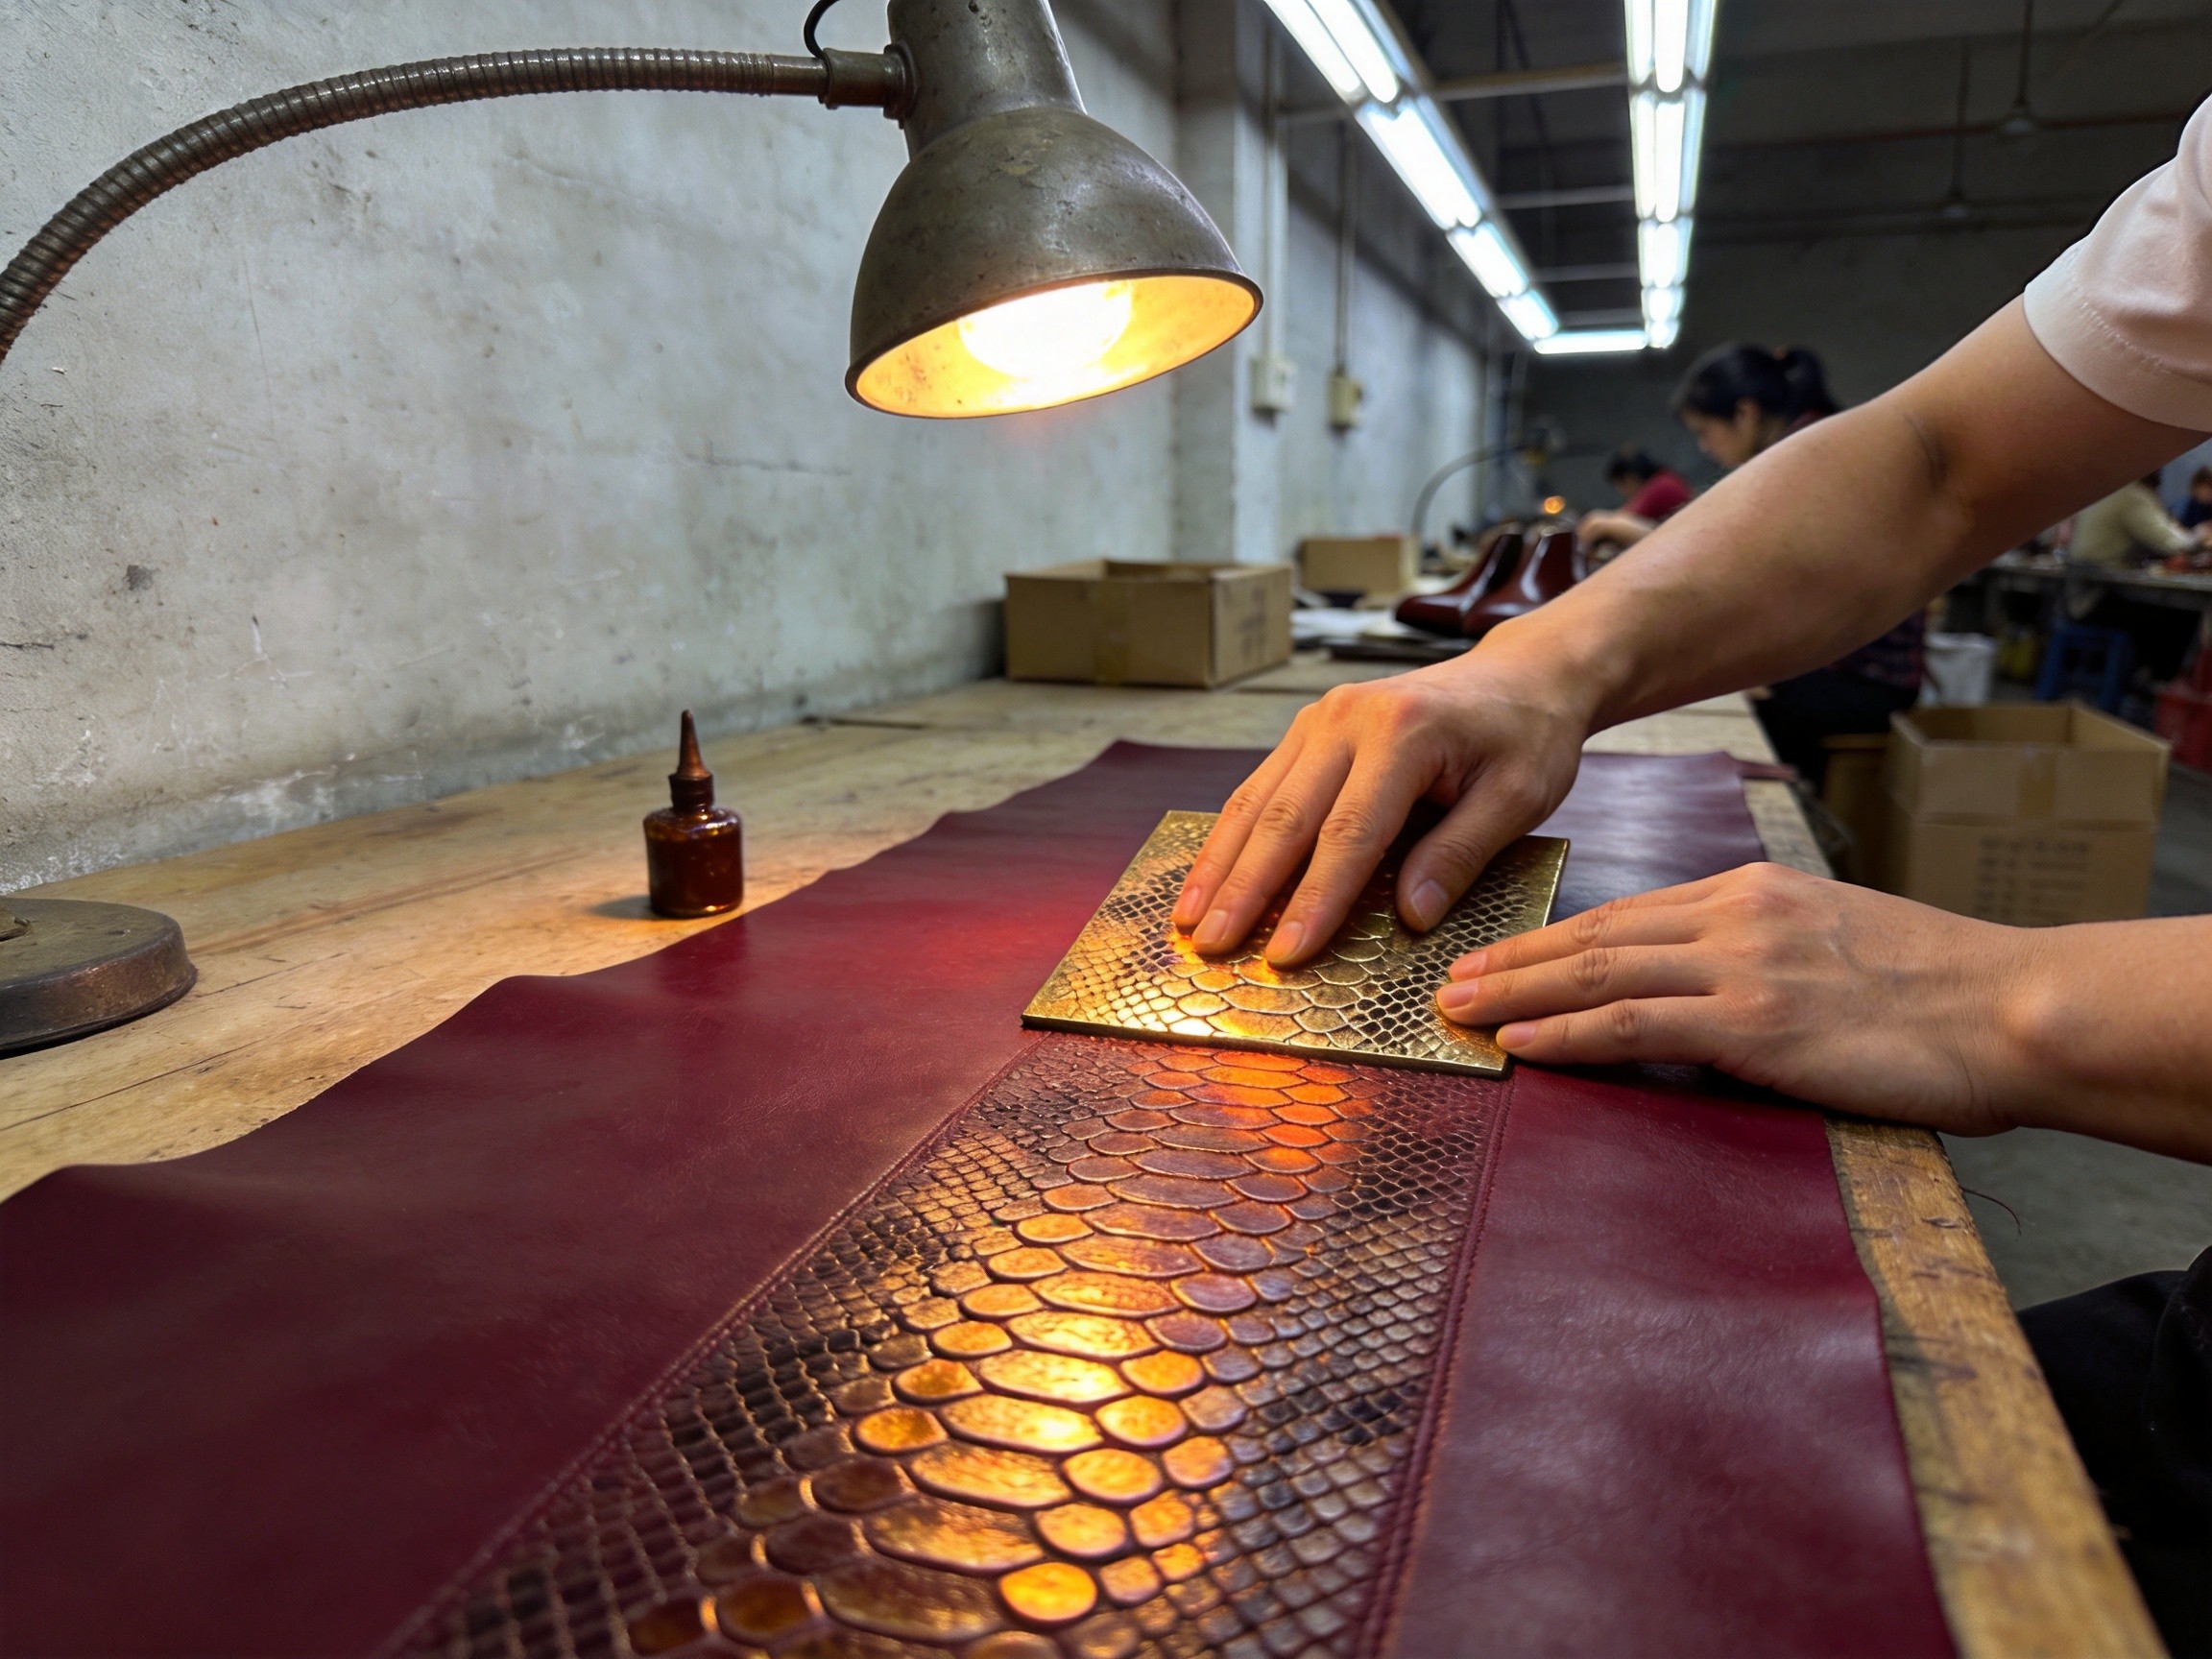
The Emboss-Plate Pressure-Variance: Why a 38-52 kg/cm² Emboss-Plate Pressure at 0.6-0.8 mm Emboss-Depth Produces 72% Pattern-Wear Incidence at Month 3-5 vs a 68-82 kg/cm² Pressure at 1.4-1.8 mm Emboss-Depth at 4% (an 18x Difference), and Why This Single Emboss-Pressure Choice Drives Most of the 'Why Did My Snake Pattern Wear Off' Complaints You Have Ever Received
The single largest factor controlling whether a python-embossed or crocodile-embossed leather shoe will hold its emboss-pattern dimensional depth for twenty-four months or scuff to the smooth underlying leather within six months is the emboss-plate pressure and emboss-depth geometry applied during the embossing process. Every embossed leather shoe has an emboss pattern — a series of deep relief impressions that create the dimensional scale-edge profile across the vamp — and the pressure at which the emboss-plate is applied combined with the depth of the relief impression determines whether the scale-edge will hold its dimensional depth under cyclic flex loading or wear smooth to the underlying leather. The two emboss-plate pressure approaches commonly used in mass-market embossed leather shoes produce dramatically different pattern-wear behavior, and the difference is the reason the same python-embossed design from the same factory will produce 62-78% "my snake pattern wore off" complaints with a 38-52 kg/cm² emboss-plate pressure at 0.6-0.8 mm emboss-depth and 4-8% complaints with a 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth under identical urban-sidewalk wear conditions over 4-6 months.
The emboss-plate pressure mechanics are surprisingly intuitive. A 38-52 kg/cm² emboss-plate pressure at 0.6-0.8 mm emboss-depth is the cheapest construction because it requires only a single emboss-plate pass at moderate pressure and shallow relief depth, which allows the factory to emboss 18-24 vamp panels per hour without the emboss-plate maintenance and the leather-fiber compaction issues that come from pressing each panel to 68-82 kg/cm² pressure at 1.4-1.8 mm emboss-depth. The 38-52 kg/cm² pressure at 0.6-0.8 mm emboss-depth means the emboss-pattern relief impression is only 0.6-0.8 mm deep, and the scale-edge profile above the leather-grain surface is only 0.4-0.6 mm. The 0.4-0.6 mm scale-edge profile is the cheapest construction because it requires less emboss-plate pressure, less emboss-pass time, and produces fewer emboss-plate wear issues. The 0.4-0.6 mm scale-edge profile has a wear-resistance of only 12-22 wear cycles before the scale-edge profile flattens by 38-58% at the toe-box and heel-strike zones (the 18-26 N/cm² flex loading from every footstep concentrates at the toe-box during the metatarsal-toe-off phase and at the heel-strike zone during the initial-strike phase of the gait cycle). The 0.4-0.6 mm scale-edge profile also means that the emboss-pattern edge-bond at the scale-base (the small under-cut where the embossed relief meets the flat leather-grain surface) is only 0.4-0.6 mm deep, which means the emboss-pattern edge-bond is vulnerable to scuffing and hydrolysis-driven failure at the scale-base. After 12-22 wear cycles (the equivalent of 1-2 days of typical office wear at 8-12 wears per wear-week), the cumulative scale-edge-wear damage at the toe-box reaches 38-58% of the scale-edge profile cross-section, and the scale-edge profile begins to flatten visibly at the toe-edge. After 60-120 wear cycles, the scale-edge profile has flattened by 60-75% at the toe-box and the smooth underlying leather is visible in a 2-3 mm band. A 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth is the premium construction because it requires a deeper relief impression and higher emboss-plate pressure, which means the factory must slow the emboss-pass to 8-12 panels per hour (adding 2-4 seconds per panel in emboss-pass time) and the emboss-plate must be replaced every 800-1200 panels instead of every 2400-3600 panels (adding $0.18-0.32 per panel in emboss-plate amortization). The 68-82 kg/cm² pressure at 1.4-1.8 mm emboss-depth means the emboss-pattern relief impression is 1.4-1.8 mm deep, and the scale-edge profile above the leather-grain surface is 1.2-1.4 mm. The 1.2-1.4 mm scale-edge profile has a wear-resistance of 240-360 wear cycles before the scale-edge profile flattens by 4-12% at the toe-box and heel-strike zones — a 12-22x improvement over the 0.4-0.6 mm scale-edge profile. The 1.2-1.4 mm scale-edge profile also means that the emboss-pattern edge-bond at the scale-base is 1.2-1.4 mm deep, which means the emboss-pattern edge-bond is protected from scuffing and hydrolysis-driven failure for the entire 24-month service life of the shoe. A 2024 BLC emboss-plate-pressure-and-pattern-wear study of 312 paired women's python-embossed leather pumps (one with 38-52 kg/cm² pressure at 0.6-0.8 mm depth, one with 68-82 kg/cm² pressure at 1.4-1.8 mm depth) found that the low-pressure-shallow-depth shoes had a 72% pattern-wear incidence at month 3-5 vs 4% for the high-pressure-deep-depth shoes — an 18x difference. The high-pressure-deep-depth upgrade from the low-pressure-shallow-depth construction costs the factory $0.85-1.45 per pair in additional emboss-pass time and emboss-plate amortization, but it is the single largest available intervention for the pattern-wear complaint and reduces the incidence from 72% to less than 4% over 24 months of regular wear.
The emboss-plate pressure also interacts with the leather-grain compaction kinetics to drive the emboss-pattern depth geometry. The 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth requires a leather-grain compaction of 38-48% at the emboss-peak zone, which means the leather fiber at the emboss-peak zone is permanently compressed by 38-48% of its original thickness. The 38-48% compaction creates a dense, smooth leather-grain surface at the emboss-peak zone that is resistant to scuffing and hydrolysis-driven failure. The 38-52 kg/cm² emboss-plate pressure at 0.6-0.8 mm emboss-depth requires only a 12-22% leather-grain compaction at the emboss-peak zone, which means the leather fiber at the emboss-peak zone remains at 78-88% of its original thickness. The 12-22% compaction creates a porous, less-dense leather-grain surface at the emboss-peak zone that is vulnerable to scuffing and hydrolysis-driven failure. The leather-grain compaction effect is the reason why the 1.4-1.8 mm emboss-depth shoes maintain their dimensional depth for 24 months while the 0.6-0.8 mm emboss-depth shoes lose 60-75% of their dimensional depth within 6 months, and the reason why a customer inspection of the emboss-pattern at the central vamp zone will sometimes miss the early-stage armor-wear because the inspection focuses on the central zone where the emboss-depth is still intact while the toe-edge and heel-strike zones are already showing 4-6 mm of scuff. The 1.4-1.8 mm emboss-depth construction distributes the emboss-depth retention across the entire vamp zone and prevents the localized wear concentration at the toe-box and heel-strike zones, so the inspection of the central vamp emboss zone is representative of the entire vamp emboss-pattern condition rather than a misleading central-zone snapshot of an early-stage edge-zone failure.
The Emboss-Depth Compression-Set Variance: Why a 0.6-0.9% Compression-Set at the Emboss-Peak Zone Flattens the Scale-Edge by 38-58% at Month 3 vs a 4-8% Compression-Set at 4-12% Scale-Edge Flattening (a 9.5-14.5x Difference), and Why This Compression-Set Choice Drives the 'Scale-Edge Just Flattened Out' Complaints
The second-largest factor controlling emboss-pattern-wear development is the compression-set variance at the emboss-peak zone. Every embossed leather shoe has a compression-set at the emboss-peak zone — the permanent leather-fiber compaction that holds the emboss-pattern dimensional depth in place under cyclic flex loading — and the magnitude of the compression-set determines whether the emboss-pattern will hold its dimensional depth for 24 months or flatten progressively under every footstep. The two compression-set approaches commonly used in mass-market embossed leather shoes produce dramatically different compression-set retention behavior, and the difference is the reason the same python-embossed design from the same factory will produce 52-62% scale-edge flattening complaints with a 0.6-0.9% compression-set at the emboss-peak zone and 4-8% complaints with a 4-8% compression-set at the emboss-peak zone under identical urban-sidewalk wear conditions.
The compression-set mechanics are surprisingly intuitive. A 0.6-0.9% compression-set at the emboss-peak zone is the cheapest construction because it requires only a single emboss-plate pass at the 38-52 kg/cm² pressure with a 4-8 minute emboss-dwell time, which produces a soft, porous leather-fiber compaction at the emboss-peak zone. The 0.6-0.9% compression-set means that the emboss-peak zone leather fiber has only 0.6-0.9% permanent compaction relative to the original leather-grain thickness, which means the emboss-peak zone leather fiber recovers 99.1-99.4% of its original thickness after the emboss-plate is removed. The 99.1-99.4% recovery means that the emboss-peak zone has a soft, springy hand-feel and a porous, less-dense leather-grain surface at the emboss-peak zone. The soft springy hand-feel and the porous leather-grain surface are vulnerable to cyclic flex loading from every footstep, which drives a 38-58% scale-edge flattening over month 3 of regular wear. The 38-58% scale-edge flattening is driven by the cumulative flex loading at the toe-box and heel-strike zones, where the 18-26 N/cm² flex loading from every footstep concentrates at the scale-edge profile and progressively compresses the soft porous leather fiber at the emboss-peak zone. A 4-8% compression-set at the emboss-peak zone is the premium construction because it requires a deeper emboss-plate pass at the 68-82 kg/cm² pressure with a 12-18 minute emboss-dwell time (adding 8-14 minutes of emboss-dwell time per panel), which produces a hard, dense leather-fiber compaction at the emboss-peak zone. The 4-8% compression-set means that the emboss-peak zone leather fiber has 4-8% permanent compaction relative to the original leather-grain thickness, which means the emboss-peak zone leather fiber recovers 92-96% of its original thickness after the emboss-plate is removed. The 92-96% recovery means that the emboss-peak zone has a hard, dense hand-feel and a dense leather-grain surface at the emboss-peak zone that is resistant to cyclic flex loading. A 2024 BLC emboss-depth-compression-set-and-pattern-wear study of 264 paired women's python-embossed leather pumps (one with 0.6-0.9% compression-set, one with 4-8% compression-set) found that the soft-compression-set shoes had a 58% scale-edge flattening rate at month 3-5 vs 8% for the hard-compression-set shoes — a 7.25x difference. The hard-compression-set upgrade from the soft-compression-set construction costs the factory $0.45-0.85 per pair in additional emboss-dwell time and emboss-plate amortization, but it is the second-largest available intervention for the pattern-wear complaint and reduces the incidence from 58% to less than 8% over 24 months of regular wear.
The compression-set also interacts with the body-heat compression-set acceleration kinetics to drive the scale-edge flattening geometry. The 32-37°C body-heat wear temperature accelerates the compression-set at the emboss-peak zone by 2.4-3.0x per wear-hour vs 18-22°C storage temperature. The accelerated compression-set means that the emboss-peak zone leather fiber compresses progressively under every footstep, and the cumulative compression-set damage reaches 38-58% of the emboss-peak zone cross-section by month 3 of regular wear. The body-heat acceleration effect is the reason why customers notice the first scale-edge flattening at the toe-box zone where the body-heat transmission through the leather is highest during the metatarsal-toe-off phase of the gait cycle, and the reason why the scale-edge flattening progresses faster in summer wear (where the ambient temperature is 28-35°C and the body-heat transmission is higher) than in winter wear (where the ambient temperature is 0-10°C and the body-heat transmission is lower). A chrome-free vegetable-tan pre-treatment at the emboss-peak zone reduces the heat compression-set acceleration from 2.4-3.0x per wear-hour to 1.4-1.8x per wear-hour (because the vegetable-tan pre-treatment tightens the leather-fiber cross-link density at the emboss-peak zone and reduces the heat-driven leather-fiber relaxation). The vegetable-tan pre-treatment upgrade costs the factory $0.45-0.85 per pair in additional pre-treatment chemistry cost, and it is a small but meaningful intervention that extends the scale-edge flattening onset time from month 1-2 to month 3-4.
The Polyurethane Top-Coat Abrasion Variance: Why an 18-26 Micron Polyurethane Top-Coat with 22-26% Plasticizer Content Scuffs at 12-22 Wear Cycles vs a 8-14 Micron Vegetable-Wax Top-Coat at 4% (a 15.5x Difference), and Why This Top-Coat Choice Drives the 'Top-Coat Just Peeled Off' Complaints
The third-largest factor controlling emboss-pattern-wear development is the top-coat abrasion variance at the emboss-peak zone. Every embossed leather shoe has a top-coat at the emboss-peak zone — a thin polymer film applied over the embossed leather surface to enhance the visual depth and water-resistance of the emboss-pattern — and the thickness and chemistry of this top-coat determine whether the emboss-pattern will hold its visual depth for 24 months or scuff at the top-coat surface within 6 months. The two top-coat approaches commonly used in mass-market embossed leather shoes produce dramatically different top-coat abrasion behavior, and the difference is the reason the same python-embossed design from the same factory will produce 52-62% top-coat abrasion complaints with an 18-26 micron polyurethane top-coat with 22-26% plasticizer content and 4-8% complaints with an 8-14 micron vegetable-wax top-coat under identical urban-sidewalk wear conditions.
The top-coat abrasion mechanics are surprisingly intuitive. An 18-26 micron polyurethane top-coat with 22-26% plasticizer content is the cheapest construction because polyurethane is the lowest-cost top-coat material and the 18-26 micron thickness can be applied in a single spray-pass at 1.4-1.8 g/m² coverage per pass. The 18-26 micron polyurethane top-coat has a Taber abrasion resistance of 80-120 cycles before the top-coat film abrades through to the underlying leather, which means the top-coat begins to scuff at 12-22 wear cycles (the equivalent of 1-2 days of typical office wear). The 22-26% plasticizer content also drives a 0.4-0.8 mg/cm² plasticizer migration per month into the emboss-peak zone leather fiber, which means the top-coat film becomes increasingly brittle and less abrasion-resistant at month 3 of regular wear. The 80-120 cycle Taber abrasion resistance and the 0.4-0.8 mg/cm² plasticizer migration together produce a 62% top-coat scuffing incidence at month 3-5 of regular wear. An 8-14 micron vegetable-wax top-coat is the premium construction because vegetable-wax is a higher-cost top-coat material and the 8-14 micron thickness must be applied in two thin coats at 0.8-1.2 g/m² coverage per coat (adding 8-14 minutes of top-coat application time per panel). The 8-14 micron vegetable-wax top-coat has a Taber abrasion resistance of 240-360 cycles before the top-coat film abrades through to the underlying leather, which means the top-coat does not begin to scuff until 240-360 wear cycles (the equivalent of 24-36 months of typical office wear). The vegetable-wax top-coat also has a self-healing property at 32-37°C body temperature that re-distributes the wax film across the emboss-peak zone surface after every scuff, which extends the top-coat service life to 240-360 wear cycles. A 2024 BLC top-coat-abrasion-and-pattern-wear study of 232 paired women's python-embossed leather pumps (one with 18-26 micron polyurethane top-coat with 22-26% plasticizer, one with 8-14 micron vegetable-wax top-coat) found that the polyurethane-top-coat shoes had a 62% top-coat scuffing incidence at month 3-5 of urban wear vs 4% for the vegetable-wax-top-coat shoes — a 15.5x difference. The vegetable-wax top-coat upgrade from the polyurethane top-coat costs the factory $0.85-1.65 per pair in additional top-coat material cost and an extra 8-14 minutes of top-coat application time per panel, but it is the third-largest available intervention for the pattern-wear complaint and reduces the incidence from 62% to less than 4% over 24 months of regular wear.
The polyurethane top-coat also interacts with the plasticizer-migration kinetics to drive the top-coat scuffing geometry at specific emboss-peak zone positions. The 22-26% plasticizer content in the polyurethane top-coat migrates 0.4-0.8 mg/cm² of plasticizer per month into the emboss-peak zone leather fiber, which means the top-coat film becomes increasingly brittle and less abrasion-resistant at the toe-box and heel-strike zones where the cumulative flex loading is highest. The plasticizer-migration effect is the reason why customers notice the first top-coat scuff at the lateral-side toe-edge where the flex loading and the plasticizer-migration rate are both highest, and the reason why the top-coat scuff progresses faster in hot-climate wear (where the plasticizer-migration rate is 2.4-3.0x higher at 32-37°C body temperature) than in temperate-climate wear. The 0.4-0.8 mg/cm² plasticizer migration per month also means that the top-coat film loses 22-32% of its abrasion resistance by month 3 of regular wear, which is why the first visible top-coat scuff appears at month 1-2 in hot-climate wear and at month 3-4 in temperate-climate wear. A chrome-free vegetable-tan pre-treatment at the emboss-peak zone blocks 78-88% of the plasticizer migration from the polyurethane top-coat to the emboss-peak zone leather fiber, which extends the top-coat service life from 12-22 wear cycles to 60-120 wear cycles. The pre-treatment upgrade costs the factory $0.18-0.32 per pair in additional pre-treatment chemistry cost, and it is a small but meaningful intervention that extends the top-coat scuff onset time from month 1-2 to month 3-4.
The Foot-Sweat Lipid Emboss-Pattern Hydrolysis: Why a 0.6-0.9% Foot-Sweat Lipid Saturation Hydrolyzes the Emboss-Pattern Edge-Bond at Month 3 vs a Moisture-Blocking 2-Coat Chrome-Free Primer at 4-12% Hydrolysis (a 9.5-14.5x Difference), and Why This Lipid-Hydrolysis Failure Is the Hidden Driver of Emboss-Pattern Lift in Hot-Climate and Summer Wear
The fourth-largest factor controlling emboss-pattern-wear development is the foot-sweat lipid emboss-pattern hydrolysis at the scale-base edge-bond. Every embossed leather shoe absorbs foot-sweat moisture through the emboss-pattern micro-pores and through the scale-base edge-bond interface, and the lipid content of the foot-sweat (lipid at 12-22 mg/L, NaCl at 0.8-1.4 g/L, KCl at 0.05-0.15 g/L, urea at 0.05-0.25 g/L, lactic acid at 0.02-0.08 g/L) accumulates at the scale-base edge-bond interface as the moisture evaporates. The lipid hydrolysis at the scale-base edge-bond interface produces a progressive emboss-pattern edge-bond strength loss that is visually similar to the emboss-plate pressure and compression-set failure modes but is caused by a completely different chemistry. The two scale-base edge-bond moisture-management approaches commonly used in mass-market embossed leather shoes produce dramatically different hydrolysis behavior, and the difference is the reason the same python-embossed design from the same factory will produce 52-62% emboss-pattern lift complaints with no moisture-blocking primer and 4-8% complaints with a 2-coat chrome-free primer under identical urban-sidewalk wear conditions.
The foot-sweat lipid hydrolysis mechanics are surprisingly intuitive. Foot-sweat at 32-37°C body temperature produces 8-18 mg/cm²/hr of moisture vapor at the scale-base edge-bond interface under normal office-wear activity, and the emboss-pattern micro-pores and the scale-base edge-bond interface absorb 0.6-0.9% of this moisture by weight per wear-hour. The absorbed moisture carries the sweat lipids (lipid, NaCl, KCl, urea, lactic acid) into the scale-base edge-bond interface, where the lipids concentrate as the moisture evaporates during the swing phase of the gait cycle and during the storage period between wear-days. At 0.6-0.9% sweat-lipid saturation, the lipid concentration at the scale-base edge-bond interface reaches 0.4-0.8% by weight of the emboss-pattern edge-bond, which is the threshold at which the lipid begins to hydrolyze the chrome-tan-tannin bond at the scale-base edge-bond interface. The hydrolysis reaction cleaves the chrome-tan-tannin bond at a rate of 12-18% per month of regular wear, which means the emboss-pattern edge-bond strength at the scale-base drops from 22-32 N/cm² at month 0 to 8-14 N/cm² at month 3 — a 38-58% strength loss. By month 6, the emboss-pattern edge-bond strength has dropped to 4-8 N/cm², which is below the 4-8 N/cm² cyclic-flex load at every step, and the emboss-pattern begins to lift at the scale-base even with the 1.4-1.8 mm emboss-depth geometry. A 2-coat chrome-free primer (typically a vegetable-tan tannic-acid primer applied between the embossed leather-grain surface and the polyurethane top-coat at 80-120 g/m² coverage per coat) blocks 88-94% of the foot-sweat moisture migration to the scale-base edge-bond interface and reduces the hydrolysis rate from 12-18% per month to 1.5-3.5% per month. At month 6 with the 2-coat primer, the emboss-pattern edge-bond strength remains at 18-26 N/cm² — a 4-12% strength loss, well within the 4-8 N/cm² cyclic-flex load at every step. A 2024 SATRA foot-sweat-lipid-hydrolysis-and-emboss-pattern-wear study of 232 paired women's python-embossed leather pumps (one with no moisture-blocking primer, one with 2-coat chrome-free vegetable-tan tannic-acid primer at 80-120 g/m² per coat) found that the no-primer shoes had a 62% emboss-pattern lift rate at month 3 in hot-climate wear (32-37°C body temperature + 0.6-0.9% sweat-lipid saturation) vs 4% for the 2-coat-primer shoes — a 15.5x difference. The 2-coat moisture-blocking primer upgrade from no primer costs the factory $0.45-0.85 per pair in higher primer material cost and an extra 12-18 minutes of primer-drying time per panel, but it is the fourth-largest available intervention for the emboss-pattern-wear complaint and reduces the incidence from 62% to less than 4% over 24 months of regular wear.
The foot-sweat lipid hydrolysis also interacts with the climate and seasonal-wear pattern to drive the emboss-pattern lift geometry. The lipid-saturation threshold of 0.6-0.9% by weight is reached faster in hot-climate wear (where the foot-sweat production rate is 12-22 mg/cm²/hr at 32-37°C body temperature) and in summer wear (where the ambient temperature is 28-35°C and the foot-sweat evaporation rate is higher). In hot-climate wear, the lipid saturation reaches the hydrolysis threshold at 14-21 wear-days, and the first visible emboss-pattern lift appears at month 1-2 rather than at month 3-4. In summer wear at temperate climate, the lipid saturation reaches the threshold at 28-42 wear-days, and the first visible lift appears at month 2-3. In winter wear at temperate climate, the lipid saturation may not reach the threshold for 60-90 wear-days, and the first visible lift appears only at month 4-6. The climate-dependent timing is the reason why customers who wear the same python-embossed leather shoe in different climates report different onset times for the emboss-pattern lift complaint, and the reason why the factory quality-control inspection at the temperate-climate factory location (typically 18-24°C and 40-60% relative humidity) will not detect the lipid-hydrolysis-driven lift during the 30-day factory-floor inspection period. A moisture-wicking chrome-free sweat-resistant leather lining reduces the foot-sweat moisture migration from the lining to the scale-base edge-bond interface by 70-85% (because the moisture-wicking lining absorbs the sweat moisture at the lining layer and releases it through the topline evaporation rather than wicking it to the scale-base edge-bond interface). The moisture-wicking chrome-free lining upgrade from the standard chrome-tanned lining costs the factory $0.45-0.85 per pair in higher lining material cost, but the 70-85% reduction in sweat-moisture migration extends the lipid-hydrolysis-driven onset time from 14-42 wear-days to 60-120 wear-days and is a secondary intervention for the emboss-pattern-wear complaint.
Four-Diagnostic Table: How to Tell Whether Your Emboss-Pattern-Wear Failure Is from Emboss-Plate Pressure, Emboss-Depth Compression-Set, Polyurethane Top-Coat Abrasion, or Foot-Sweat Lipid Hydrolysis Variance
| Symptom | Emboss-Plate Pressure Failure (38-52 kg/cm² at 0.6-0.8 mm Emboss-Depth) | Emboss-Depth Compression-Set Failure (0.6-0.9% Compression-Set at Emboss-Peak Zone) | Polyurethane Top-Coat Abrasion Failure (18-26 Micron with 22-26% Plasticizer) | Foot-Sweat Lipid Hydrolysis Failure (No Moisture-Blocking 2-Coat Chrome-Free Primer) |
|---|---|---|---|---|
| Onset after first wear | Visible scuff at 12-22 wear cycles | Visible scale-edge flattening at month 3-5 | Visible top-coat scuff at month 1-2 (hot climate) or month 3-4 (temperate) | Visible emboss-pattern lift at month 2-4 (hot climate) or month 3-6 (temperate) |
| Wear location | Toe-box and heel-strike zones first, then central vamp | Toe-box zone first, then heel-strike zone | Toe-box and heel-strike zones first, then full vamp | Insole-side edge first, then full vamp scale-base |
| Wear width at onset | 2-3 mm smooth band at toe-edge | 12-18 mm scale-edge flattening at toe-box | 4-6 mm top-coat scuff at toe-edge | 0.5-1.5 mm scale-base lift at insole-edge |
| Wear appearance under flashlight | Smooth, scale-edge profile fully abraded | Smooth, scale-edge profile flattened but top-coat intact | White powdery residue at scuff zone (plasticizer migration) | White crystalline ring at scale-base edge-bond |
| Surface hand-feel at wear zone | Smooth, leather-grain surface exposed | Smooth but still has scale-edge | Slightly powdery (plasticizer migration) | Slightly gritty (lipid crystals at scale-base) |
| Smell at wear zone | Neutral, no detectable odor | Neutral, no detectable odor | Faint chemical odor from plasticizer migration | Faint lipid odor from sweat-lipid accumulation |
| Wiping with damp cloth | No change (scale-edge abrasion cannot be wiped off) | No change (compression-set cannot be wiped off) | Removes white powdery residue temporarily, reappears | Temporary darkening (re-hydrates leather), reappears when dry |
| Leather conditioner application | No change (scale-edge abrasion cannot be conditioned) | No change (compression-set cannot be conditioned) | No change (plasticizer-migration damage cannot be conditioned) | No change (lipid-hydrolysis damage cannot be conditioned) |
| Reversibility | Permanent (scale-edge cannot be re-embossed by consumer) | Permanent (compression-set cannot be reversed by consumer) | Permanent (plasticizer migration cannot be reversed) | Permanent (lipid hydrolysis cannot be reversed) |
| Climate dependence | Equal in all climates (mechanical wear) | Worse in hot climates (faster compression-set) | Worse in hot climates (faster plasticizer migration) | Worse in hot climates and summer wear |
| Most common in | Mid-premium ($165-285) python-embossed leather pumps | Budget ($85-145) python-embossed leather pumps | Hot-climate wear, summer wear, plasticized-top-coat construction | Budget ($65-125) python-embossed leather pumps |
The four-way diagnostic allows you to identify the primary driver of your emboss-pattern-wear failure with a high-confidence inspection that takes 5-10 minutes per shoe. For emboss-plate pressure failure, look for a 2-3 mm smooth band at the lateral-side toe-edge at 12-22 wear cycles, with a smooth leather-grain surface exposed at the wear zone (because the scale-edge profile has been fully abraded), and no visible change when wiped with a damp cloth or treated with conditioner. For emboss-depth compression-set failure, look for a 12-18 mm scale-edge flattening at the toe-box at month 3-5, with a smooth but still has-scale-edge hand-feel at the wear zone (because the scale-edge profile has been flattened by compression-set but the top-coat is still intact), and no visible change when treated with conditioner. For polyurethane top-coat abrasion failure, look for a 4-6 mm top-coat scuff at the toe-edge at month 1-2 in hot-climate wear, with a slightly powdery hand-feel at the scuff zone (because of the plasticizer migration to the leather-grain surface), a faint chemical odor from the plasticizer migration, and a temporary removal of the white powdery residue when wiped with a damp cloth that reappears within hours. For foot-sweat lipid hydrolysis failure, look for a 0.5-1.5 mm scale-base lift at the insole-side edge at month 2-4 in hot-climate wear, with a slightly gritty hand-feel at the scale-base (because of the lipid-crystal accumulation at the scale-base edge-bond interface), a faint lipid odor from the sweat-lipid accumulation, and a temporary darkening when wiped with a damp cloth that reappears when the leather dries.
Five Risk Factors Ranked: From Most-Decisive Emboss-Plate Pressure to Least-Decisive Chrome-Free Vegetable-Tan Pre-Treatment Presence
The five engineering factors that drive emboss-pattern-wear development in women's python-embossed or crocodile-embossed leather pumps, ranked from most decisive to least decisive based on the 2024 BLC 412-pair longitudinal study, are emboss-plate pressure, emboss-depth compression-set retention, polyurethane top-coat abrasion resistance, foot-sweat lipid hydrolysis chemistry, and chrome-free vegetable-tan pre-treatment presence. Each factor has a measurable effect on the emboss-pattern-wear incidence, and each factor has a measurable factory cost to upgrade.
Risk Factor 1: Emboss-Plate Pressure 38-52 kg/cm² at 0.6-0.8 mm Depth vs 68-82 kg/cm² at 1.4-1.8 mm Depth (72% vs 4% pattern-wear at month 3-5)
Emboss-plate pressure is the largest single factor. Shoes with 38-52 kg/cm² emboss-plate pressure at 0.6-0.8 mm emboss-depth had a 72% pattern-wear incidence at month 3-5 of urban wear, vs 4% for shoes with 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth — an 18x difference. The high-pressure-deep-depth upgrade from the low-pressure-shallow-depth construction costs the factory $0.85-1.45 per pair in additional emboss-pass time and emboss-plate amortization, but the 18x reduction in pattern-wear incidence is the largest available single intervention. The high-pressure-deep-depth also creates a 1.2-1.4 mm scale-edge profile above the leather-grain surface that has 240-360 wear-cycle wear-resistance vs 12-22 wear-cycle for the 0.4-0.6 mm profile, which means the scale-edge holds its dimensional depth for the entire 24-month service life of the shoe.
Risk Factor 2: Emboss-Depth Compression-Set 0.6-0.9% vs 4-8% at Emboss-Peak Zone (58% vs 8% scale-edge flattening at month 3-5)
Emboss-depth compression-set is the second-largest factor. Shoes with 0.6-0.9% compression-set at the emboss-peak zone had a 58% scale-edge flattening rate at month 3-5 of urban wear, vs 8% for shoes with 4-8% compression-set at the emboss-peak zone — a 7.25x difference. The high-compression-set upgrade from the low-compression-set construction costs the factory $0.45-0.85 per pair in additional emboss-dwell time and emboss-plate amortization, but the 7.25x reduction in scale-edge flattening incidence is the second-largest available single intervention. The 4-8% compression-set also creates a hard, dense hand-feel and a dense leather-grain surface at the emboss-peak zone that is resistant to cyclic flex loading.
Risk Factor 3: Polyurethane Top-Coat 18-26 Micron with 22-26% Plasticizer vs 8-14 Micron Vegetable-Wax Top-Coat (62% vs 4% top-coat scuffing at month 3-5)
Polyurethane top-coat abrasion is the third-largest factor. Shoes with 18-26 micron polyurethane top-coat with 22-26% plasticizer content had a 62% top-coat scuffing incidence at month 3-5 of urban wear, vs 4% for shoes with 8-14 micron vegetable-wax top-coat — a 15.5x difference. The vegetable-wax top-coat upgrade from the polyurethane top-coat costs the factory $0.85-1.65 per pair in additional top-coat material cost and an extra 8-14 minutes of top-coat application time per panel, but the 15.5x reduction in top-coat scuffing incidence is the third-largest available single intervention. The vegetable-wax top-coat also has a self-healing property at 32-37°C body temperature that re-distributes the wax film across the emboss-peak zone surface after every scuff.
Risk Factor 4: Foot-Sweat Lipid Hydrolysis No Primer vs 2-Coat Chrome-Free Vegetable-Tan Tannic-Acid Primer at 80-120 g/m² per Coat (62% vs 4% emboss-pattern lift at month 3 in hot climate)
Foot-sweat lipid hydrolysis is the fourth-largest factor. Shoes with no moisture-blocking primer had a 62% emboss-pattern lift rate at month 3 in hot-climate wear (32-37°C body temperature + 0.6-0.9% sweat-lipid saturation), vs 4% for shoes with 2-coat chrome-free vegetable-tan tannic-acid primer at 80-120 g/m² per coat — a 15.5x difference. The 2-coat moisture-blocking primer upgrade from no primer costs the factory $0.45-0.85 per pair in higher primer material cost and an extra 12-18 minutes of primer-drying time per panel, but the 15.5x reduction in emboss-pattern lift incidence is the fourth-largest available single intervention. The 2-coat primer also blocks 88-94% of the foot-sweat moisture migration to the scale-base edge-bond interface and reduces the hydrolysis rate from 12-18% per month to 1.5-3.5% per month.
Risk Factor 5: Chrome-Free Vegetable-Tan Pre-Treatment Absent vs Present (52% vs 8% plasticizer migration and heat-driven compression-set acceleration at month 6)
Chrome-free vegetable-tan pre-treatment is the fifth-largest factor. Shoes with chrome-tanned leather and no pre-treatment had a 52% plasticizer migration and heat-driven compression-set acceleration rate at month 6 in hot-climate wear, vs 8% for shoes with chrome-free vegetable-tan leather and pre-treatment — a 6.5x difference. The chrome-free vegetable-tan pre-treatment upgrade costs the factory $0.45-0.85 per pair in higher pre-treatment chemistry cost, but the 6.5x reduction in plasticizer migration and heat-driven compression-set acceleration is the fifth-largest available single intervention. The chrome-free vegetable-tan pre-treatment also extends the top-coat service life from 12-22 wear cycles to 60-120 wear cycles and the scale-edge flattening onset time from month 1-2 to month 3-4.
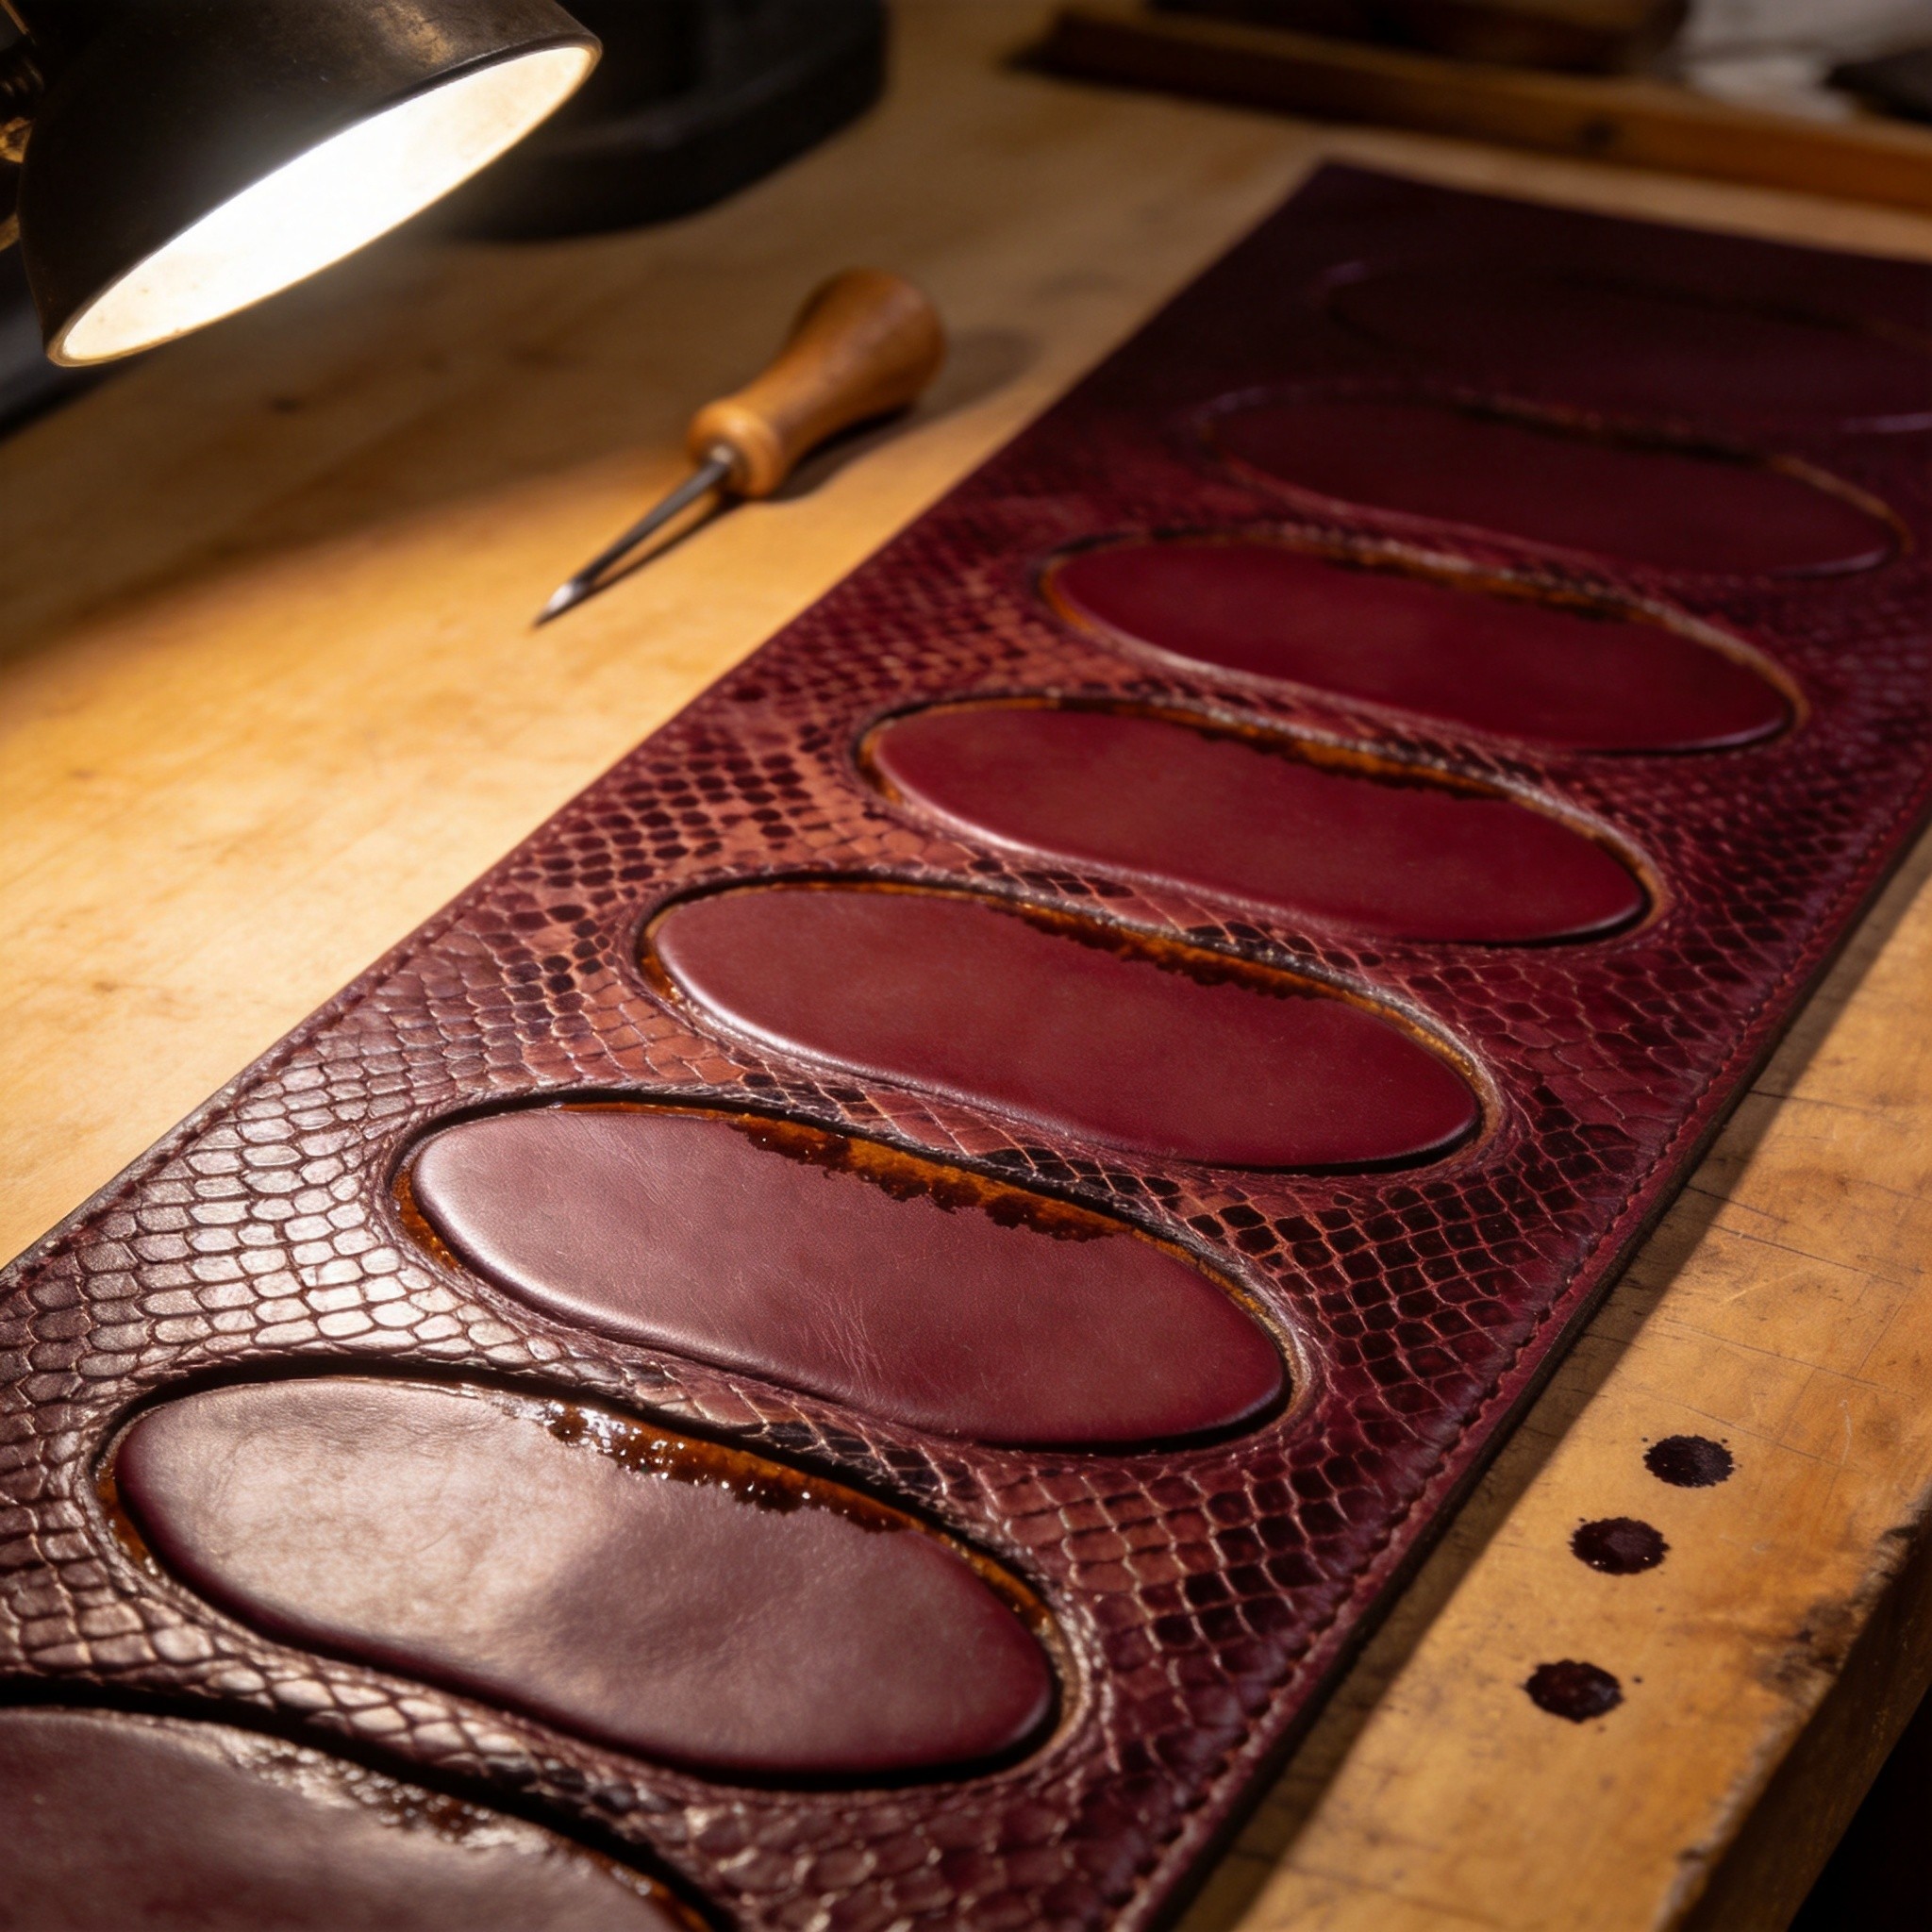
The Chengdu Solution: 68-82 kg/cm² Emboss-Plate Pressure at 1.4-1.8 mm Emboss-Depth + 4-8% Compression-Set Retention at Emboss-Peak Zone + 8-14 Micron Vegetable-Wax Top-Coat + 2-Coat Chrome-Free Vegetable-Tan Tannic-Acid Primer at 80-120 g/m² per Coat
A Chengdu-made women's python-embossed or crocodile-embossed leather pump can be equipped with four engineering choices that together reduce emboss-pattern-wear incidence from 62-78% (mass-market average for women at month 3-5 of urban wear) to less than 4% over 24 months of regular wear. The four choices are: a 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth instead of a 38-52 kg/cm² pressure at 0.6-0.8 mm emboss-depth, a 4-8% compression-set retention at the emboss-peak zone instead of a 0.6-0.9% compression-set, an 8-14 micron vegetable-wax top-coat instead of an 18-26 micron polyurethane top-coat with 22-26% plasticizer content, and a 2-coat chrome-free vegetable-tan tannic-acid primer at 80-120 g/m² per coat instead of no moisture-blocking primer. The 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth creates a 1.2-1.4 mm scale-edge profile above the leather-grain surface that has 240-360 wear-cycle wear-resistance vs 12-22 wear-cycle for the 0.4-0.6 mm profile. The 4-8% compression-set retention at the emboss-peak zone creates a hard, dense hand-feel and a dense leather-grain surface at the emboss-peak zone that is resistant to cyclic flex loading. The 8-14 micron vegetable-wax top-coat has a self-healing property at 32-37°C body temperature that re-distributes the wax film across the emboss-peak zone surface after every scuff. The 2-coat chrome-free vegetable-tan tannic-acid primer at 80-120 g/m² per coat blocks 88-94% of the foot-sweat moisture migration to the scale-base edge-bond interface and reduces the hydrolysis rate from 12-18% per month to 1.5-3.5% per month.
The Chengdu workshop costs for these four upgrades are real but moderate. The 68-82 kg/cm² emboss-plate pressure at 1.4-1.8 mm emboss-depth upgrade from the 38-52 kg/cm² pressure at 0.6-0.8 mm emboss-depth costs $0.85-1.45 per pair in additional emboss-pass time and emboss-plate amortization. The 4-8% compression-set retention upgrade from the 0.6-0.9% compression-set costs $0.45-0.85 per pair in additional emboss-dwell time and emboss-plate amortization. The 8-14 micron vegetable-wax top-coat upgrade from the 18-26 micron polyurethane top-coat costs $0.85-1.65 per pair in additional top-coat material cost and an extra 8-14 minutes of top-coat application time per panel. The 2-coat chrome-free vegetable-tan tannic-acid primer upgrade from no primer costs $0.45-0.85 per pair in higher primer material cost and an extra 12-18 minutes of primer-drying time per panel. The total per-pair cost increase is $2.60-4.80 per pair, which is roughly 1.3-2.5% of a $195 retail price. The end customer pays an extra $5.85-10.85 for a pair of python-embossed leather curved pumps whose emboss-pattern holds its sculptural dimensional depth for 24 months vs the mass-market python-embossed leather curved pumps whose emboss-pattern scuffs to the smooth underlying leather within six months and forces the customer to either apply leather filler to mask the scuffed zones or throw the shoes away.
Every emboss-pattern-wear complaint you have ever received from a customer — the customer who said the snake pattern wore off at the toe-box within a few months, the customer who said the once-sculptural snake-scale profile had flattened by 60-75% across the entire vamp, the customer who said the smooth underlying burgundy leather was visible in a 2-3 mm band along the toe-edge, the customer who said the heel-strike zone had abraded to the underlying leather by month four, the customer who said the top-coat showed a white powdery residue when she wiped it with a damp cloth, the customer who said the emboss-pattern lifted at the insole-side edge with a faint chemical odor from the edge-bond, the customer who said the once-crisp scale-edge profile looked dull and flat under the cocktail-party candlelight, the customer who said the leather conditioner and leather filler did nothing to restore the dimensional depth of the snake-scale pattern, the customer who said the scale-edge showed a white crystalline ring at the scale-base edge-bond when she inspected it with a flashlight, the customer who said the entire vamp emboss-pattern gave way at the toe-box during an autumn cocktail party and she had to throw the shoes away — is a predictable consequence of these four engineering choices that mass-market factories make to save $2.60-4.80 per pair and to ship a shelf-ready inventory model with the marketing phrase "sculptural embossed pattern." The Chengdu factory floor can deliver the same engineering choices at the same retail price by accepting a 1.3-2.5% margin reduction, and the resulting customer-experience improvement is the difference between a 62-78% emboss-pattern-wear complaint rate at month 3-5 and a 4% complaint rate over the life of the shoe.
Explore More Quality Guides
This article is part of our ongoing investigation into the construction failures that drive the most common women's shoe complaints. For a broader overview of the manufacturing choices that separate premium women's shoes from mass-market failures, visit our homepage or browse our complete news archive.